Engineered for high-intensity competition, off-ice conditioning, and team identity across North American hockey circuits.
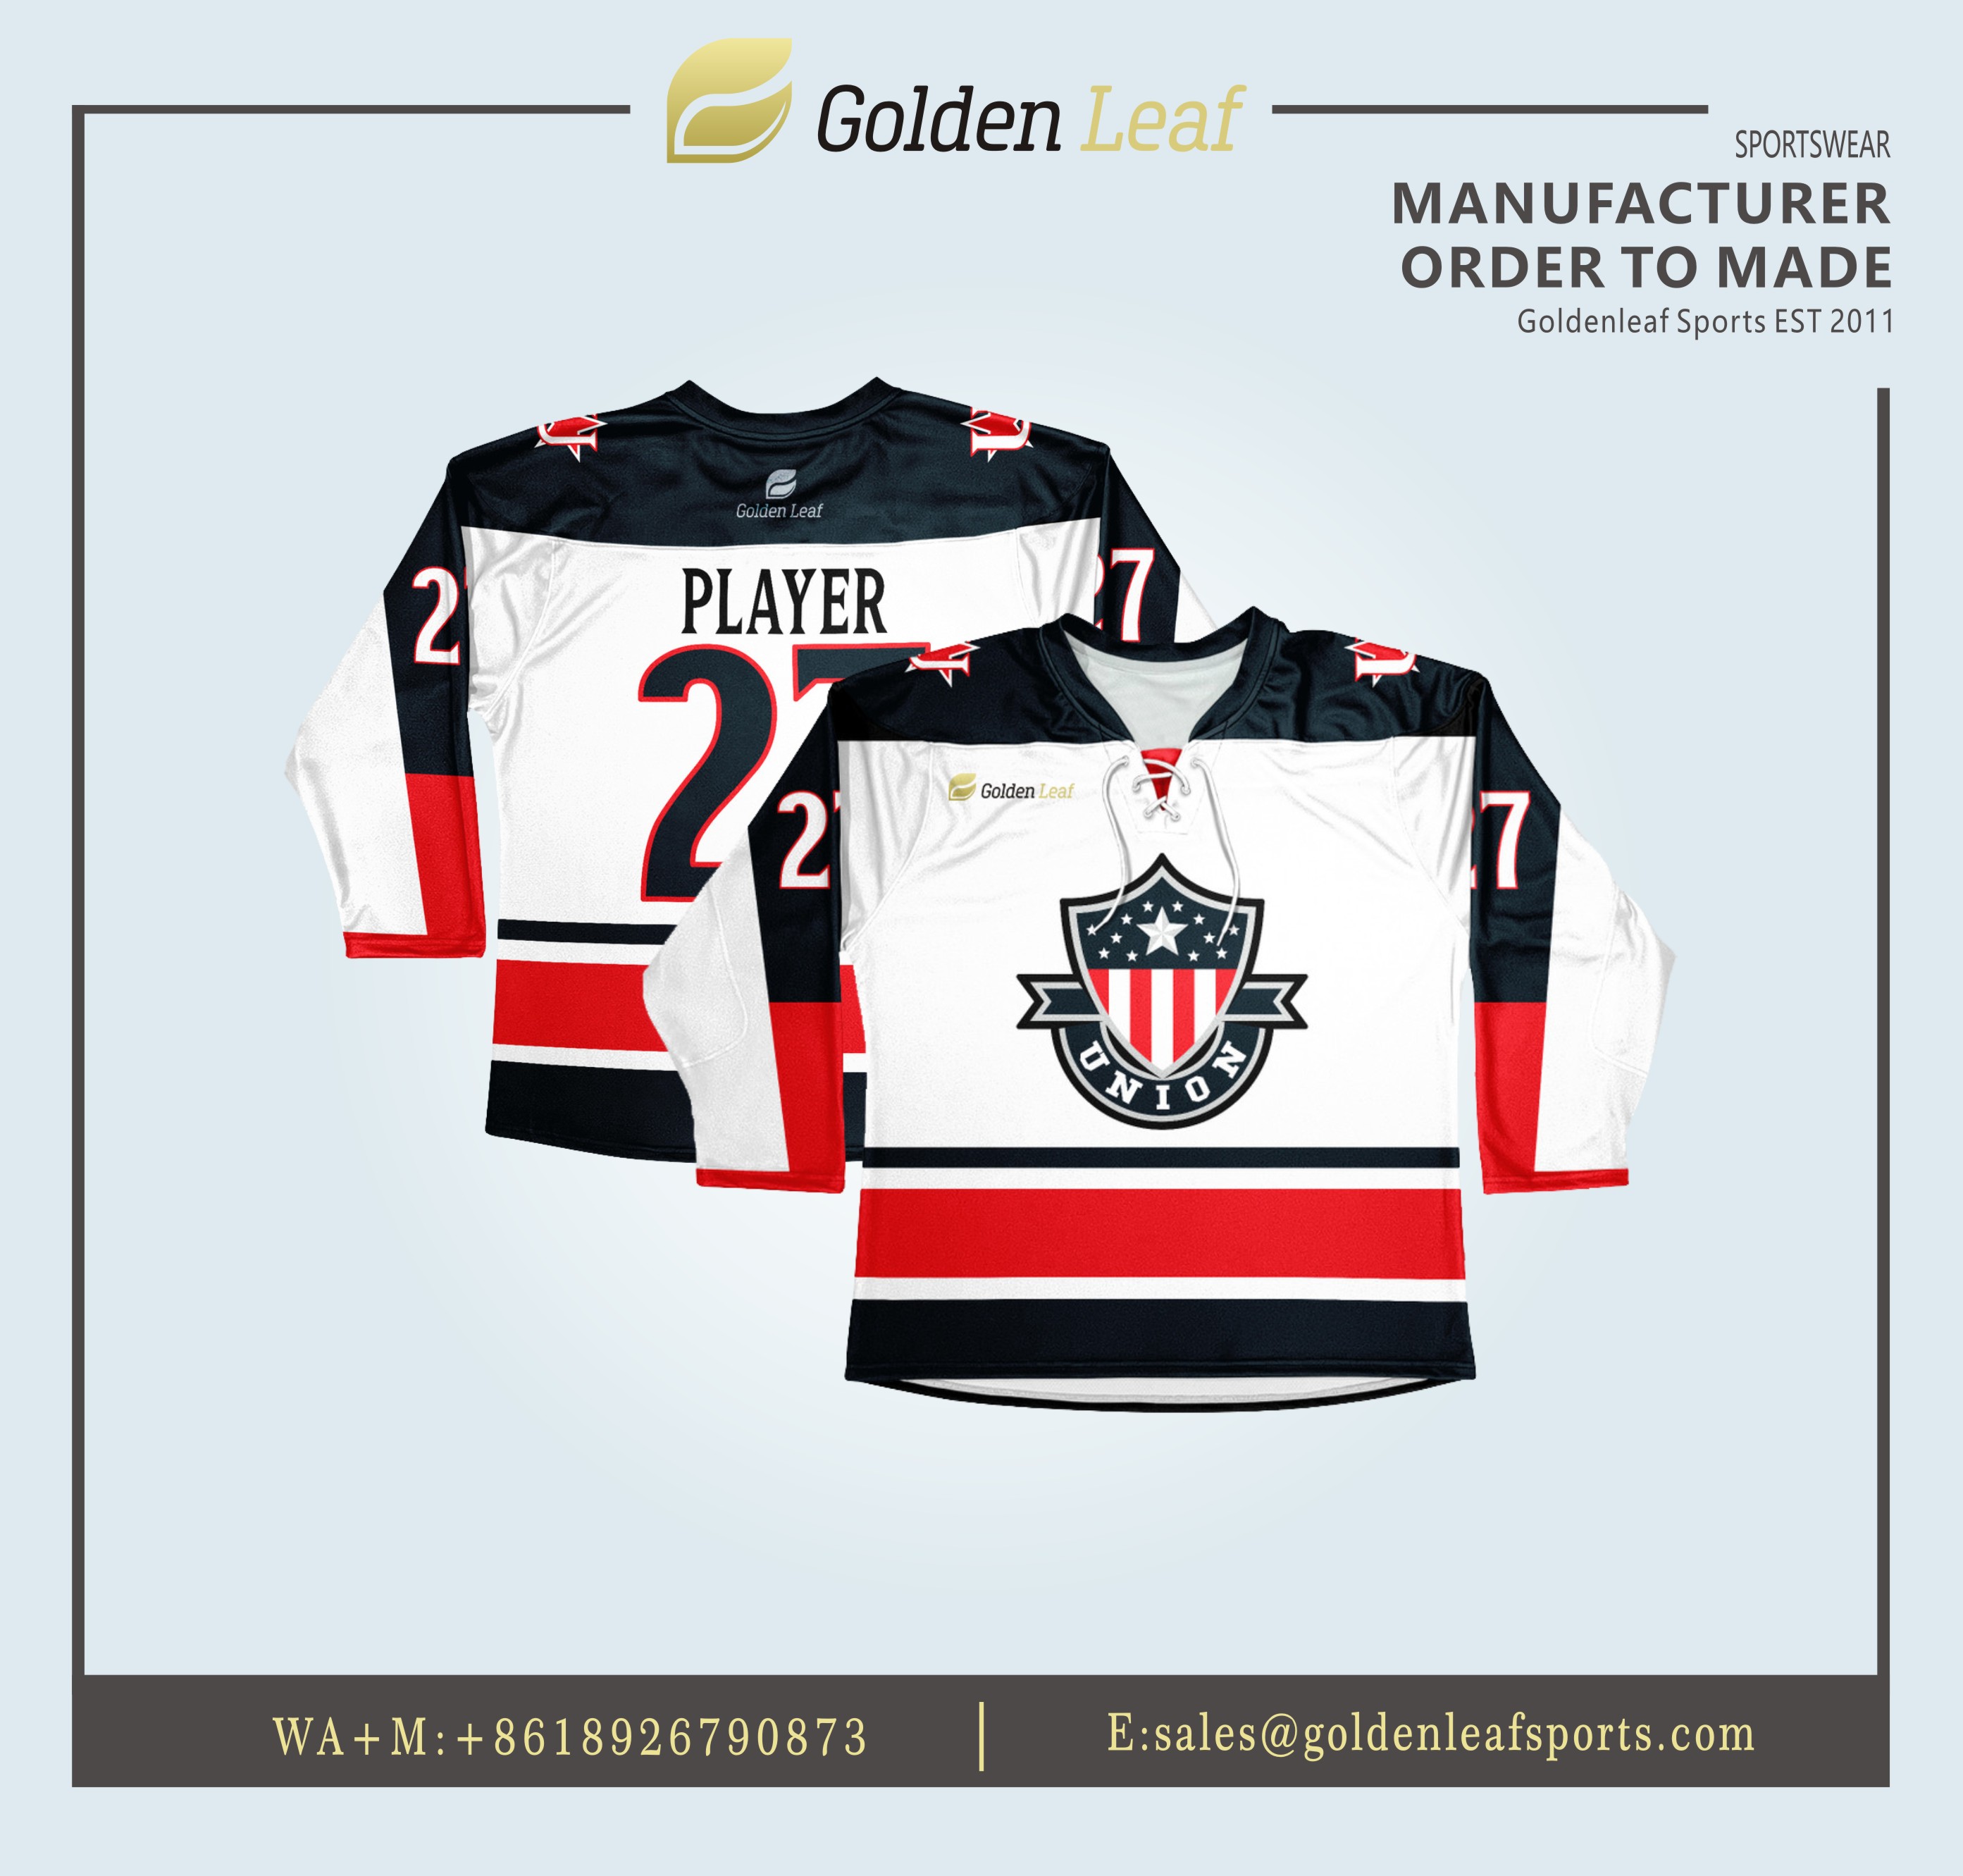
Comprehensive B2B analysis on hockey shirt market dynamics, collegiate growth, and commercial procurement models in North America.
The ice hockey ecosystem in the United States has experienced dynamic geographic expansion over the past decade. Traditional strongholds throughout the Northeast, Midwest (Minnesota, Michigan, Wisconsin), and New England have been joined by rapid grassroots adoption across the Sunbelt states, including Texas, Florida, Arizona, and Nevada. Governed by USA Hockey, over half a million registered youth, junior, and adult players compete in seasonal leagues, requiring consistent replenishments of game uniforms, practice jerseys, off-ice conditioning shirts, and fan lifestyle apparel.
For US wholesale distributors, team uniform dealers, and independent sporting goods retail chains, sourcing dependable custom hockey shirts from specialized OEM/ODM manufacturing factories is vital. Modern North American athletic programs demand shirts that withstand physical checks, blade contact, and rigorous washing cycles while delivering elite-tier breathability and thermal regulation under ice rink environmental conditions.
The institutional hockey market in the United States—comprising NCAA Division I, II, and III programs, ACHA (American Collegiate Hockey Association) club teams, USHL/NAHL junior franchises, and prestigious New England prep schools—operates under strict procurement calendars. Equipment managers and team directors seek high-precision color fidelity matching institutional Pantone specifications, custom cut-and-sew ergonomics, and specialized fabric weights ranging from 140 GSM for base layers to 220+ GSM for heavy-duty scrimmage shirts.
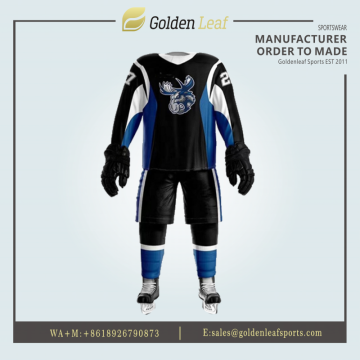
Direct factory collaboration enables US athletic organizations to bypass redundant distributor markups, securing fully personalized designs featuring sublimated tackle-twill effects, embroidered crest patches, ventilation mesh inserts, and reinforced cover-stitching at optimized wholesale pricing tiers.

Custom-knitted 100% polyester interlock and bird's-eye meshes formulated to optimize capillary action, drawing moisture away from the athlete's skin during high-intensity shifts.

Utilizing high-grade eco-friendly Italian inks that fuse directly into synthetic microfibers at 210°C, ensuring graphics never crack, peel, fade, or compromise jersey ventilation.

Empowering American B2B clients to run risk-free roster replenishment, single-player customized replacement shirts, and limited-edition tournament event drops without minimum order roadblocks.
How cutting-edge manufacturing aligns with commercial use cases in the North American sporting goods market.
Modern hockey training extends far beyond the frozen surface. Plyometric conditioning, synthetic ice shooting labs, slide-board workouts, and gym training have transformed hockey shirts into multi-functional athletic performance tops. American hockey training centers and travel programs require custom off-ice shirts that offer high four-way mechanical stretch, anti-odor silver ion fabric treatments, and ultra-lightweight breathability.
Sustainability has transitioned from a niche preference to a core procurement criterion among US municipal leagues, university athletic boards, and modern sporting apparel brands. Leading factories now integrate rPET (recycled polyethylene terephthalate) yarns derived from post-consumer plastic bottles into high-performance hockey shirts, reducing carbon footprint while upholding maximum tensile durability.
Automated vector pattern grading and AI-enhanced sublimation template generators allow US clients to transition from creative digital mockup to production-ready dye-cut panels in minutes. This digital integration shortens sampling turnaround to under 7 calendar days, enabling agile fulfillment for American tournament organizers and seasonal team sponsors requiring rapid turnarounds.
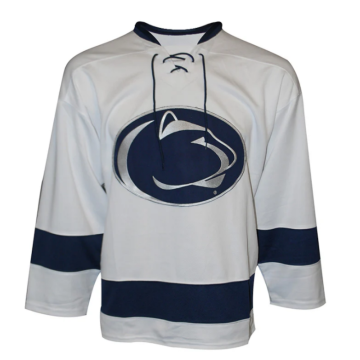
The "Reverse Retro" phenomenon in professional hockey has fueled massive commercial demand across adult recreation ("Beer Leagues") and youth clubs for vintage-inspired styling, shoulder yolk contrasts, lace-up collars, and retro color palettes rendered through crisp, ultra-high-definition digital sublimation.
High-volume uniform suites for Tier 1 AAA tournaments in Detroit, Boston, and Minneapolis requiring crisp team identifiers, sponsor badges, and player numbers.
Durable, cost-effective custom team shirts featuring humor-infused graphics, bold sublimation art, and lightweight breathability for weekend hockey warriors nationwide.
Rugged, reinforced teamwear engineered for rigorous contact play in state tournament brackets across Minnesota, Massachusetts, and North Dakota.
High-performance moisture-management workout shirts tailored for intense off-ice cardiovascular conditioning and stickhandling clinics.
GoldenLeaf Sports (ShenZhen) Co., Ltd. is specialized in designing, manufacturing and selling personalized and mainly with digital sublimation printing sportswear company with 14+ years experience on custom team uniform EST 2011. Large-scale industry and trade integration with a total area of 3000 square meters, and there are more than 160 employees in our company, 80% of colleagues are senior with rich apparel experience. Yearly output is 300K pcs. All of our products are fashionable, elegant quality.
Our products cover hockey wear, baseball uniforms, American football jerseys, board shorts, basketball uniforms, wrestling singlets, MTB shirts, volleyball wear, soccer jerseys, rugby wear, running wear, polo, t shirts, darts shirts, track suit, rash guards, cycling wear, jacket and hoodies, Lacrosse Jersey, Referee Uniform, Cricket Jersey, boxing shorts, fishing wear, yoga wear, pet clothing, arm/legging sleeves, hats, Basketball Shopping Bag etc...


End-to-end quality assurance, proprietary sublimation printing workflows, and bespoke client support.
Unlike traditional embroidery or screen printing, sublimation technology permanently integrates ink into the fibers. This means the pattern will never crack, fade, or leave a trace. You can achieve full-color, complex gradient designs, perfectly showcasing everything from fierce beast logos and cool geometric shapes to gradient colors.

Customize team names, player numbers, player names, sponsor logos, and more to create truly unique team jerseys. Our creative designers update characteristic designs all the time. We are a professional OEM & ODM manufacturer.
In order to meet the needs of individuals and follow the market trend, our company introduced the industry-leading policy "MOQ=1". After several years of careful management, we have obtained a position far ahead in the industry!
Made from high-performance 100% polyester, specifically designed for the high-intensity, high-sweat characteristics of competitive team sports.

Quick-drying and breathable properties ensure athletes stay dry, comfortable, and focused throughout the game.

Every product undergoes rigorous needle inspection to eliminate any potential safety hazards and ensure athlete safety.

Minimum order quantity is only 1 piece, supporting small-batch trial orders and large-scale purchases. Sample production is completed within 7 days.
Exporting excellence to North America and worldwide with full raw material traceability and comprehensive QC.
Main Markets: North America (25%), Oceania (15%), Eastern Europe (10%)
Main Client Types: Retailer, Wholesaler, Brand business, For private use, Manufacturer
Customization Options: Customized on demand, sample processing, graphic processing
New Products Launched in Last Year: 4,500+
R&D Engineers: 8 senior apparel designers
R&D Engineer Education Levels: 17 graduate, 10 technical school, 14 junior college across corporate technical groups
Raw material traceability support
Inspection of all finished goods
Line-level quality control
Dedicated inspectors


Our team wear made with sublimation printing with import Eco-friendly Ink, and comply with international quality standards which is greatly appreciated in a variety of markets around the world. We win a remarkable reputation from both domestic and international markets.
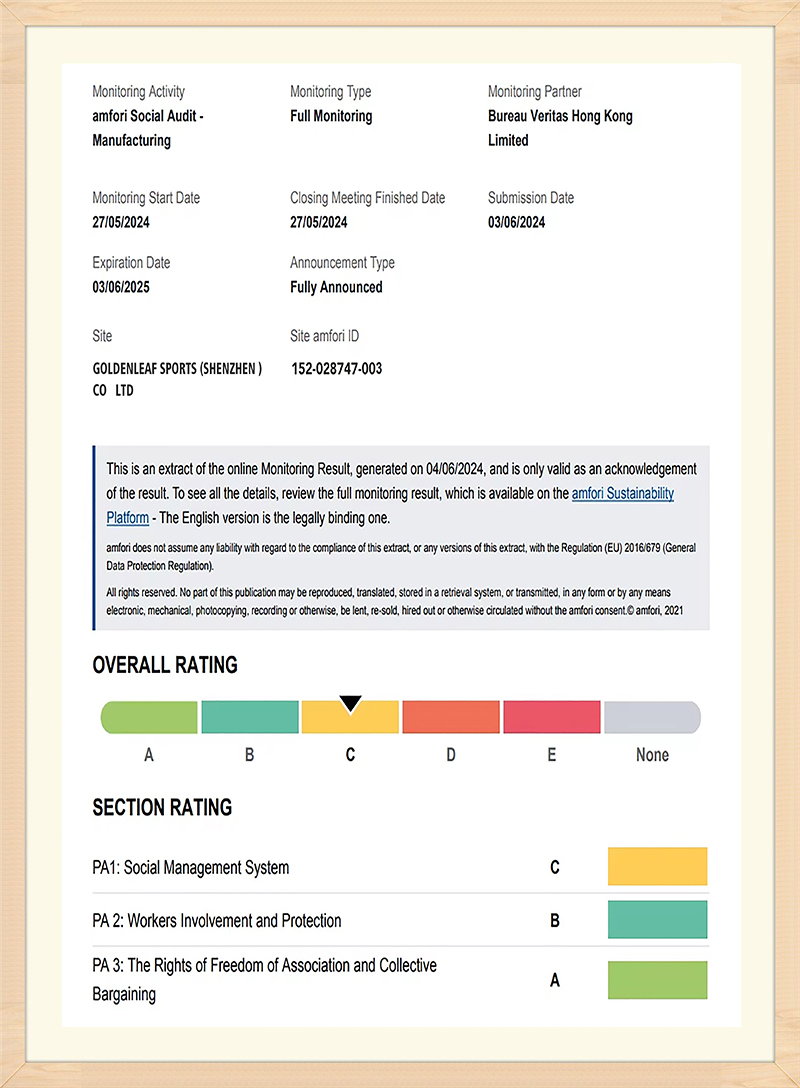
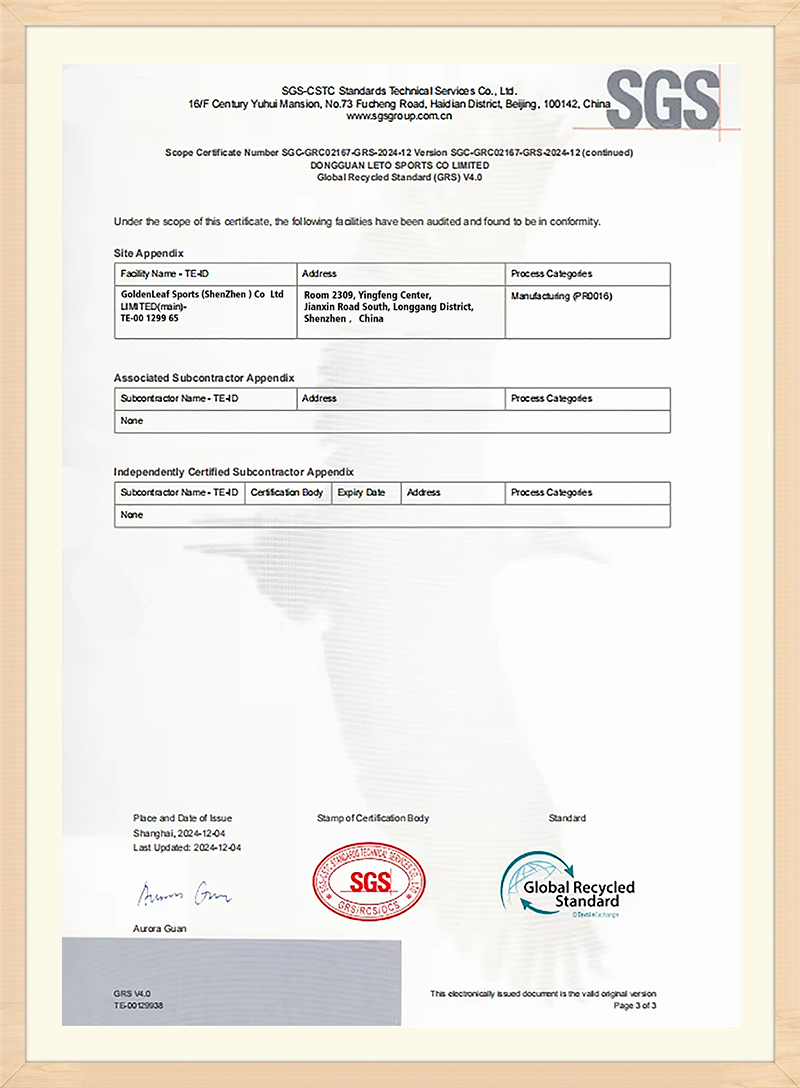
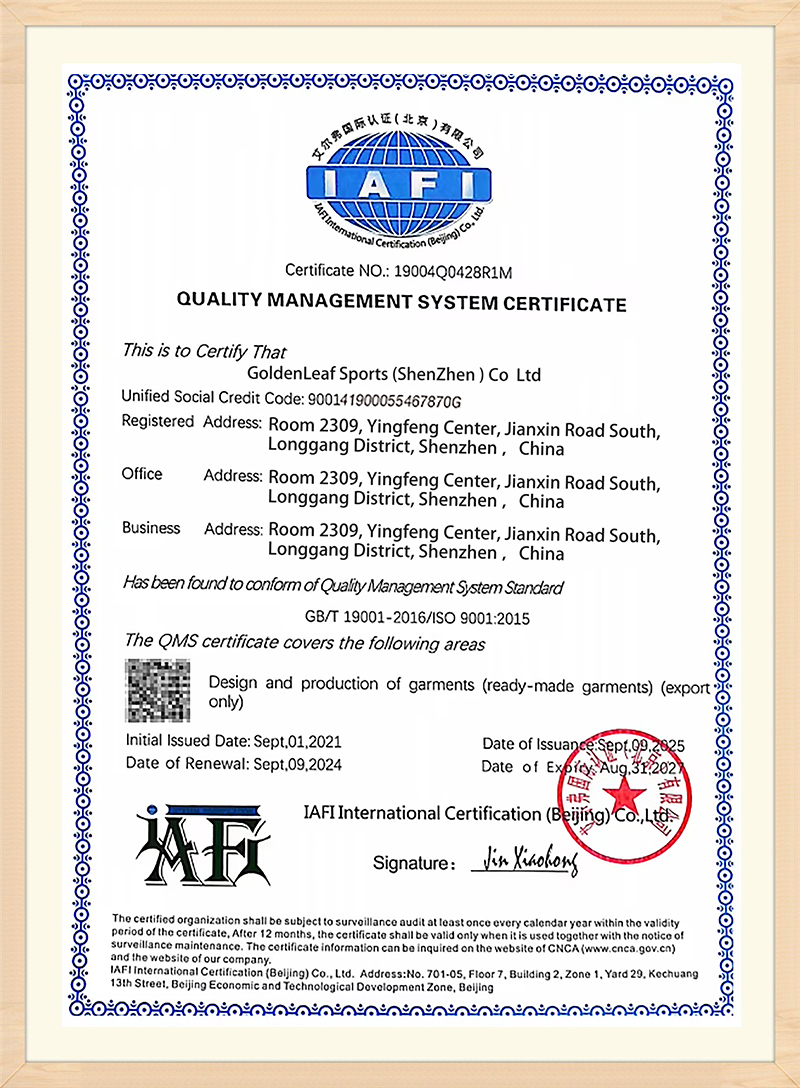
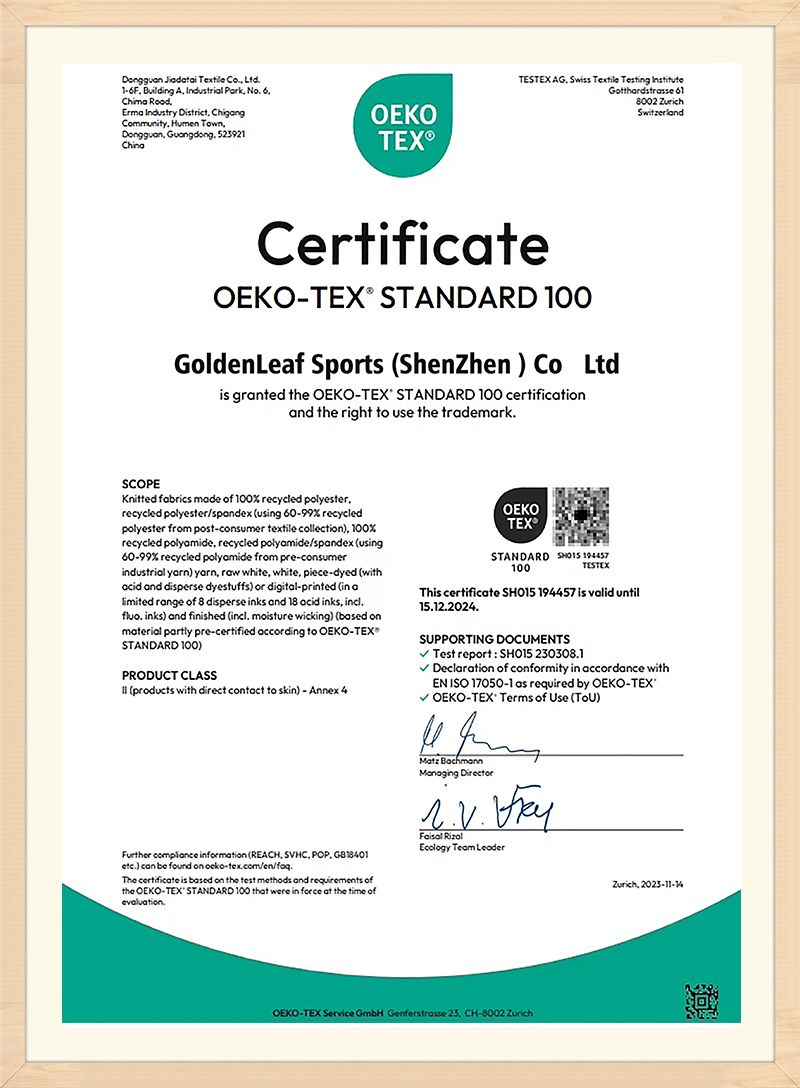
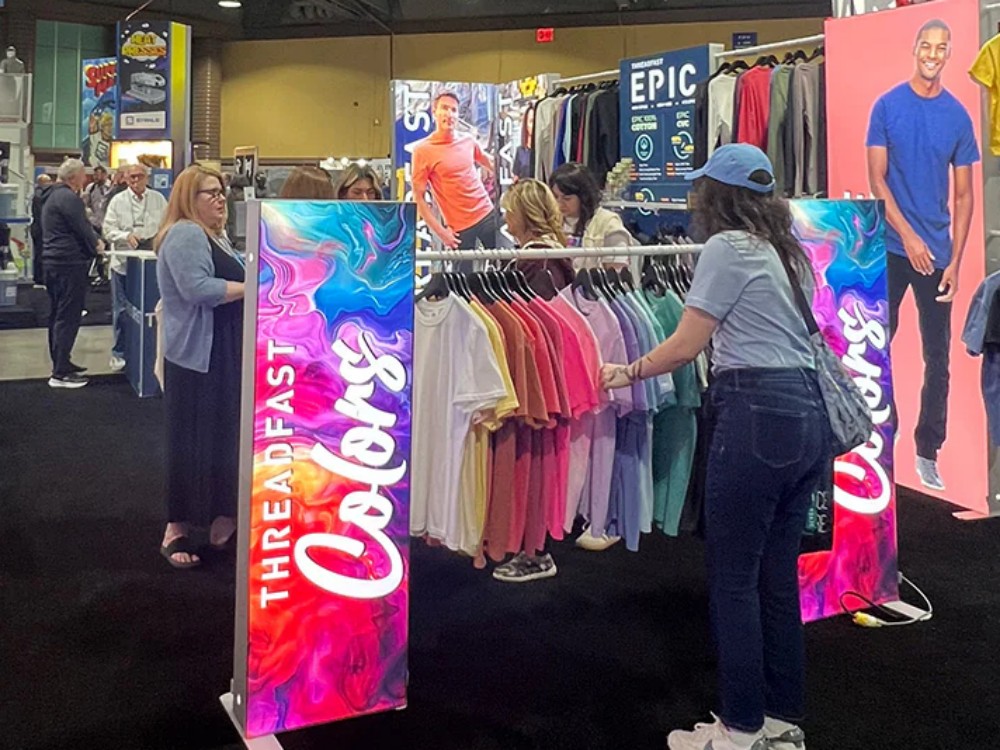
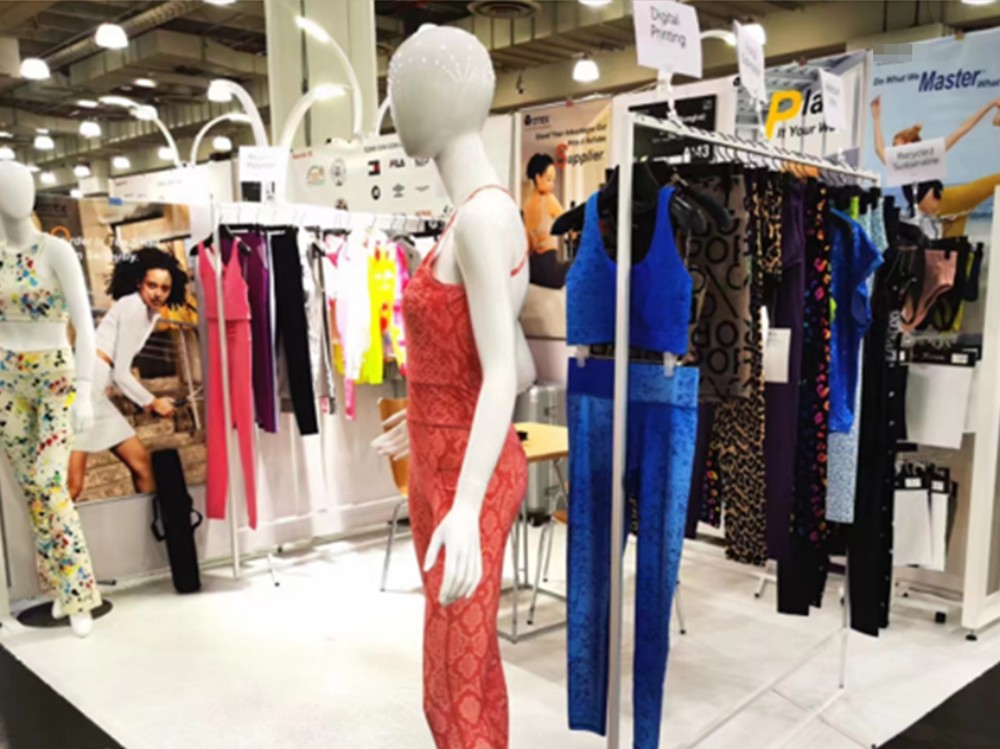
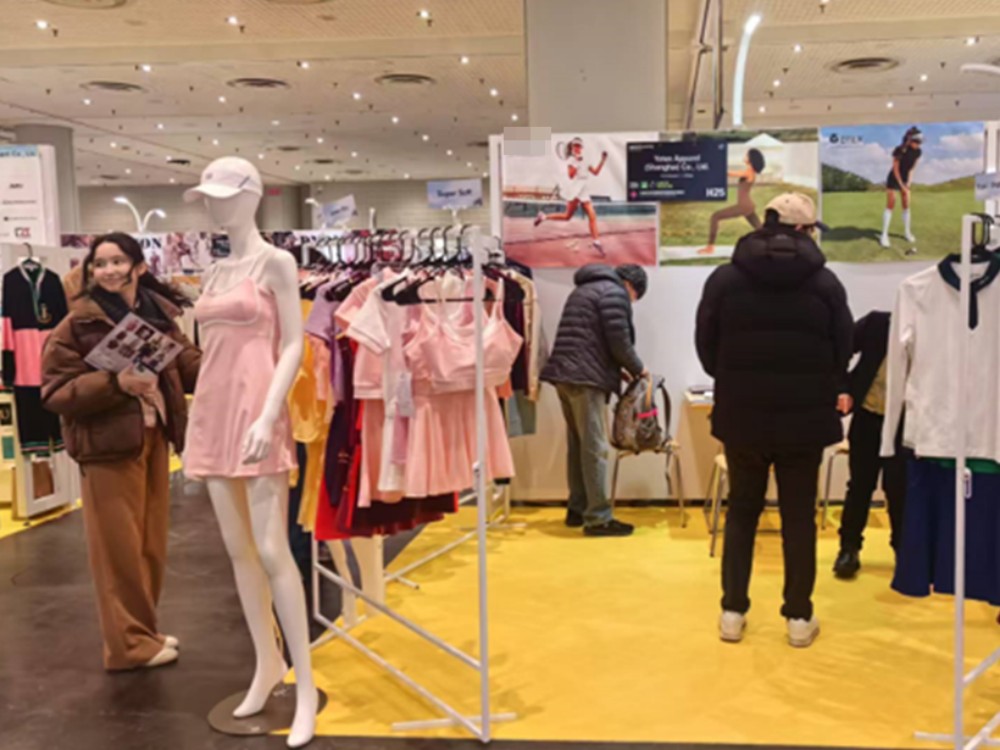
Connecting with sports apparel distributors, teamwear brands, and sporting buyers across world-class trade shows.
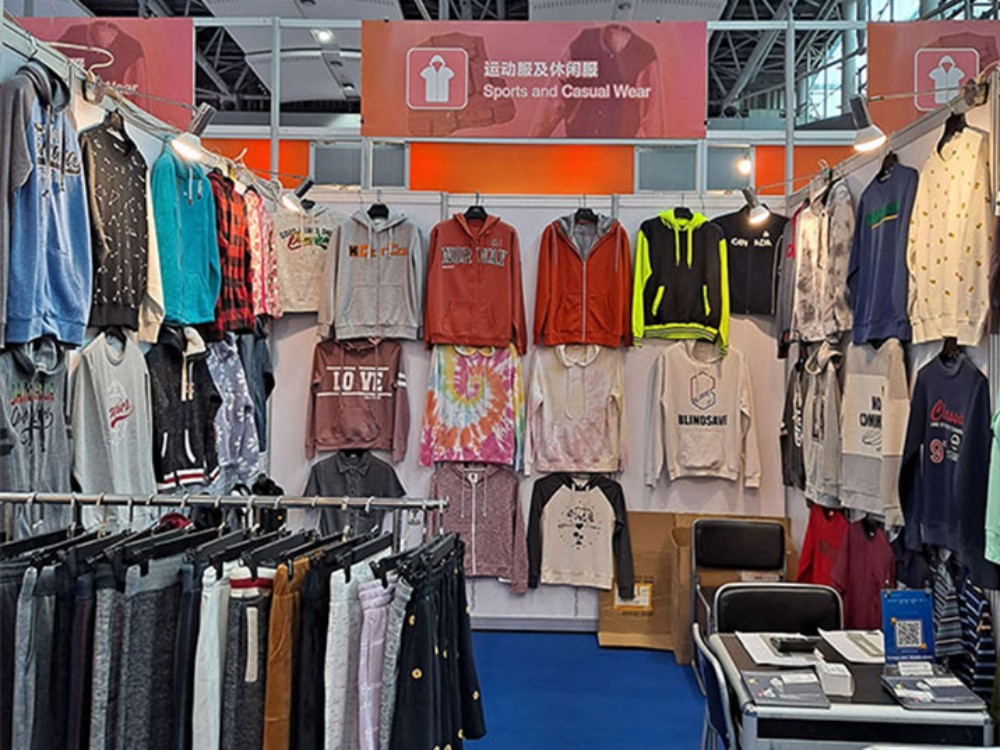
Partner directly with an established high-capacity factory. Custom teamwear samples ready in 7 days with worldwide fast-track logistics.
Browse our complete lineup of custom sublimated team uniforms, training tops, and high-performance athletic shirts.